Cleanroom / Cold
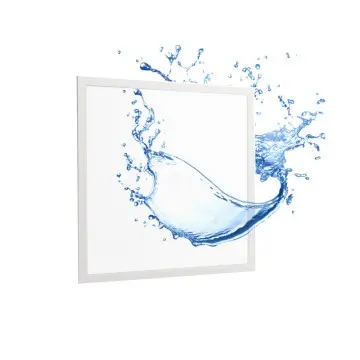
300/600/1200mm 18–60W LED Ceiling Panel Light
18–60 W
300–1200 mm
Sealed Dust-Free
Factory-direct luminaires engineered with advanced thermal management, hermetic vapor sealing, and certified for demanding sub-zero and hazardous environments.
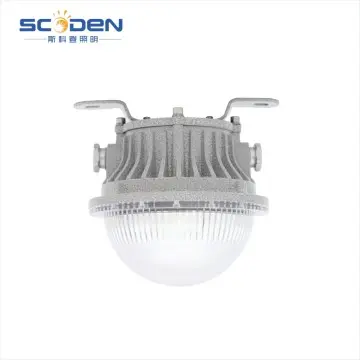
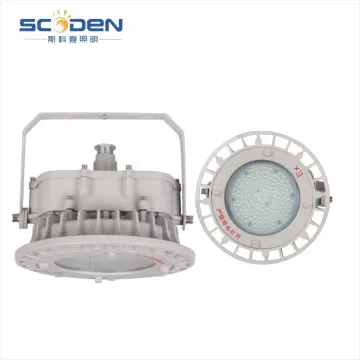
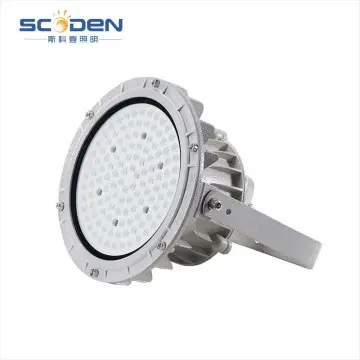
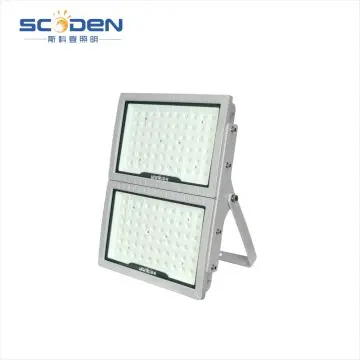
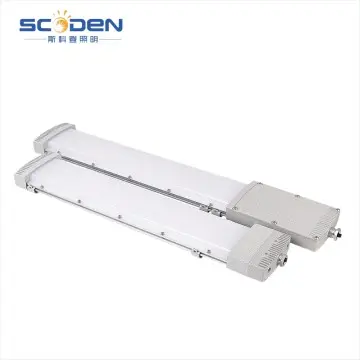
Commercial refrigerated warehousing presents severe physical challenges to standard commercial lighting. Modern cold chain logistics demand CE-certified fixtures optimized for extreme thermodynamic transitions.
When luminaires cycle off inside -25°C walk-in freezers, the internal cavity rapidly cools, dropping internal pressure and suctioning ambient moisture across sub-par gasket seals. We engineer IP66/IP69K vapor-tight silicone rings and pressure-equalizing micro-vent valves to prevent internal icing and short-circuit failures entirely.
Standard LED drivers undergo massive capacitive collapse below -15°C, resulting in high inrush currents, severe thermal throttling, and strobe flicker. Scoden utilizes low-temperature solid-state electrolyte capacitors and customized wide-voltage power supplies (AC85-265V) certified for instant cold ignition down to -40°C.
Traditional Passive Infrared (PIR) sensors register ambient thermal signatures; in frozen environments where human body thermal contrasts are obscured by thick thermal suits, PIR fails consistently. Our 5.8GHz microwave Doppler radar sensors penetrate frost, operating seamlessly to deliver 0-10V automated dimming and 75% energy savings.
International supply chain directors face strict regulatory audits. Our cold storage luminaires meet comprehensive CE directives, combining Low Voltage (LVD), Electromagnetic Compatibility (EMC), and hazardous ATEX Zone parameters.
| Evaluation Parameter | Standard Commercial Tri-Proof | Scoden Industrial Cold-Chain Grade | Compliance Advantage (CE / IEC) |
|---|---|---|---|
| Operating Range | -10°C to +40°C | -40°C to +50°C continuous | EN 60598-1 Cold Test |
| Housing Materials | Standard Recycled ABS / Polycarbonate | UV-Stabilized Bayer PC / Cast ADC12 Al | IK08 / IK10 Impact Rated |
| Ingress Protection | IP65 (Splash Resistant) | Hermetically Sealed IP66 & High-Pressure IP69K | EN 60529 Jet Wash Certified |
| Optical Efficiency | 90 – 105 lm/W | 130 – 160 lm/W (LM-80 SMD2835 / 3030) | EU ERP Ecodesign Compliant |
| Condensation Valve | None (Traps vapor causing lens fog) | Integrated ePTFE Hydrophobic Breather | Zero Internal Frost Build-up |
Headquartered in Beibaixiang Town, Yueqing, Zhejiang, Scoden Lighting leverages deep industrial cluster integration to deliver rapid OEM/ODM prototyping, full traceability, and unparalleled supply chain resilience.
Equipped with high-precision cutting machines, punching presses, automated silicone dispensing lines, and laser marking for full component batch tracing.
Every single manufactured luminaire passes 1500V-3750V dielectric withstand testing, followed by an intensive 24-hour continuous cycling and aging procedure.
From private mould tooling to Semi-Knocked Down (SKD) modular kits, we empower international partners to lower localized tariffs and establish branded assembly lines.
Our direct optical laboratory produces true goniophotometric IES and LDT files, enabling exact DIALux lighting calculations for cold store ceiling distributions.
From chemical cold rooms handling hazardous refrigerants to automated cold storage high-bay racking systems, see how our lighting ensures workplace safety and compliance.
Rapid thermal pull-down cycles generate intense surface condensation. Our seamless polycarbonate battens with IP66/IP69K ratings prevent moisture intrusion and micro-fractures during defrost heater activations.
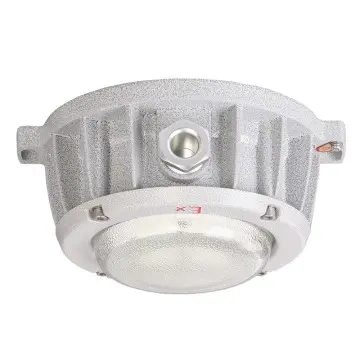
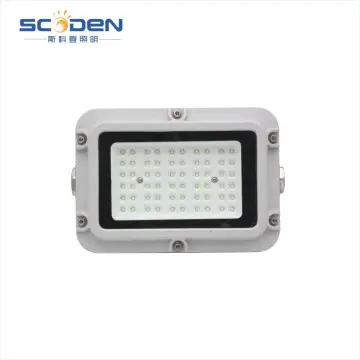
Refrigeration compressor rooms often utilize anhydrous ammonia (R717) or propane refrigerants, classifying them under ATEX Zone 1/Zone 2. Our explosion-proof floodlights and ceiling fixtures eliminate electrical spark risk.
Narrow aisles with heights exceeding 14 meters require precise narrow-beam optics (60°/90°) paired with microwave presence detection to maximize floor illuminance while trimming electrical load during idle operations.
Full documentation transparency. Complete certificate packs, ISO 9001 compliance, and third-party laboratory verification are provided with every industrial order.
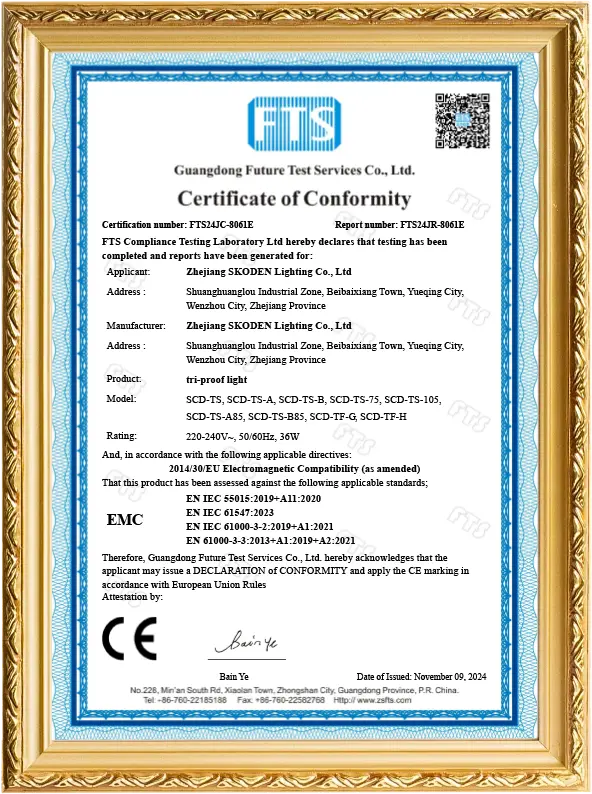
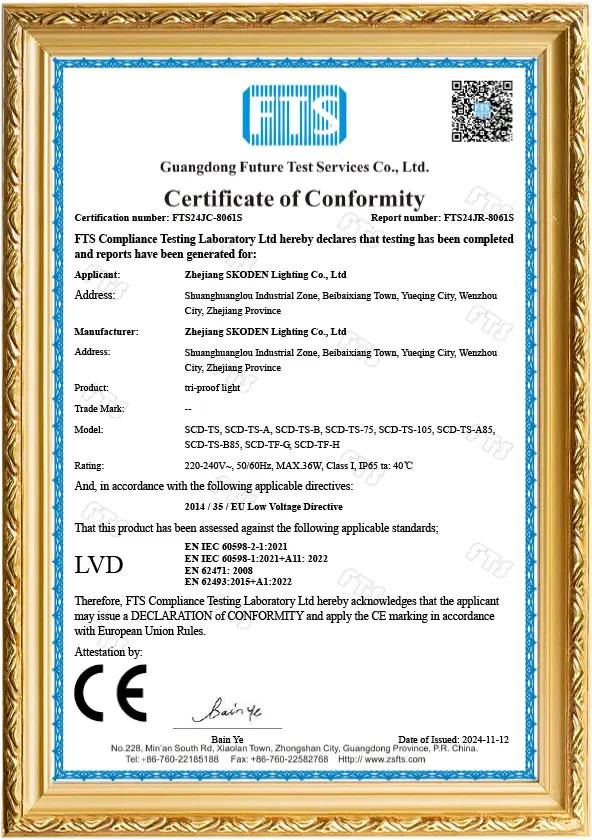
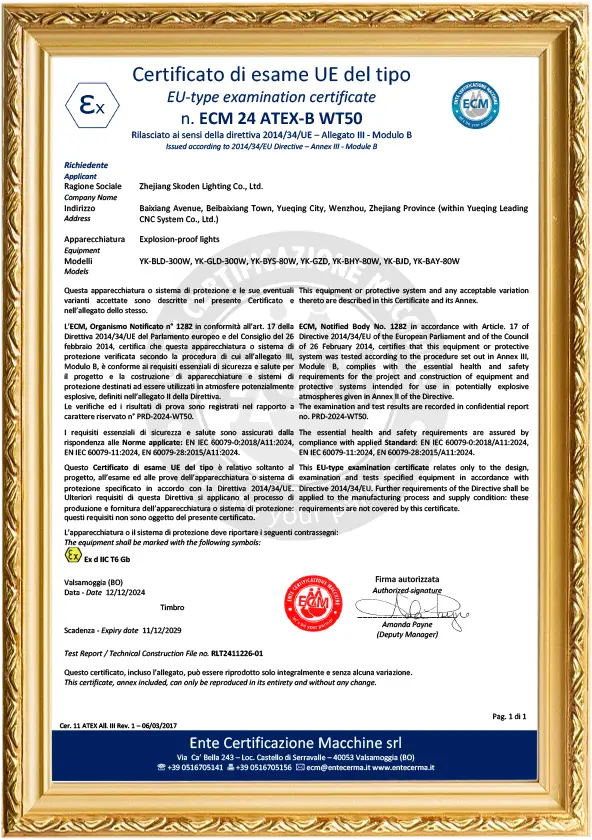
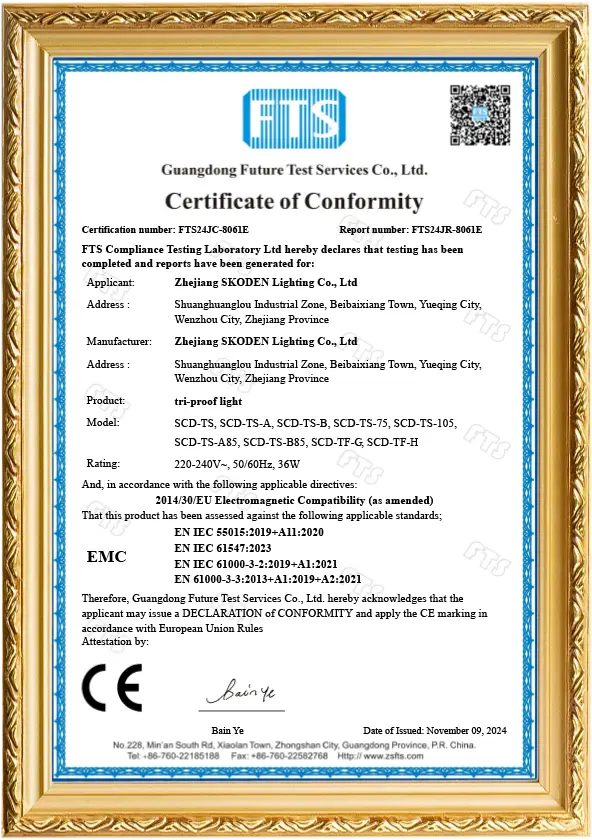
We collaborate with tier-1 component providers and global distribution networks to maintain the highest quality control and component stability.
Direct insights from our Chief Optical and Thermal Engineers addressing cold chain, ATEX compliance, and international manufacturing specifications.
Select from our field-proven luminaires, trusted by logistics hubs, hazardous industrial depots, and temperature-controlled food facilities worldwide.
Direct factory engineering consultation, verified CE/ATEX test reports, free DIALux simulations, and tailored OEM/ODM quotes within 24 hours.